Long nut-tap format
Extended reach for suitable nut-threading operations where component depth or access requires a longer tool format.
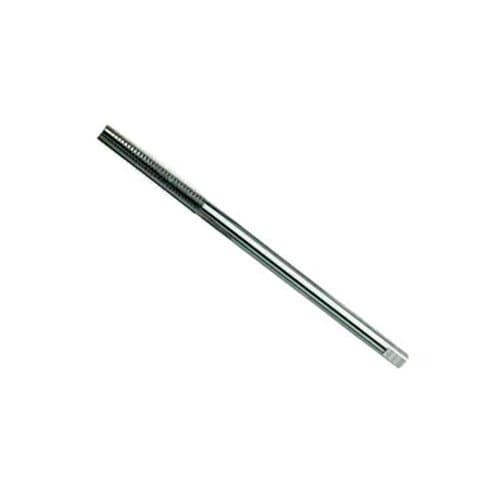
HSS Long Nut Threading Tap
Reference photo from Swastik Grand's live long-nut page. Confirm the selected configuration in your quotation.
Long nut tap manufacturer · Ludhiana, India
Extended reach for suitable nut-threading operations.
SWAGIN HSS long nut threading taps are listed for suitable internal nut-threading applications where tool reach, thread length, material, machine and quantity are reviewed together. Share the exact requirement for a standard, bulk, export or custom enquiry.
Product overview
Long nut tap selection depends on the component envelope, required reach, thread designation, nut material, machine setup, hole preparation, tolerance and production quantity.
A long nut tap is not automatically suitable for every nut-production cycle. Confirm the machine, reach, thread, material, coating and acceptance requirements in the quotation.
Application-led review
Review the tool against the actual nut, machine and process. No universal tool-life, throughput or cost-saving result is guaranteed.
Extended reach for suitable nut-threading operations where component depth or access requires a longer tool format.
Confirm machine, alignment, hole preparation, material, chip handling and production cycle before selection.
Discuss M2, M35 or M42 according to the nut material and application.
Metric, British, unified and pipe-thread requirements can be reviewed against the exact drawing.
Review 2-, 4- or 6-thread lead options against thread depth and entry conditions.
Share size-wise quantities, length, tolerance, coating, inspection and repeat-production requirements.
Technical information
These are listed product-family details. Confirm exact dimensions, reach, grade, coating, tolerance, gauge, availability and commercial terms in the quotation.
Thread families
These are enquiry options, not a live inventory claim. Send the exact component drawing where a thread designation is ambiguous.
Practical thread reference
For HSS taps and dies, metric pitch is measured in millimetres; inch threads are usually specified in TPI (threads per inch).
| Thread name | Full name / meaning | Example size |
|---|---|---|
| M – Metric Coarse | ISO metric coarse thread | M10 × 1.5 mm |
| Metric Fine / MF | ISO metric fine thread; normally marked M with pitch | M10 × 1.0 mm |
| UNC | Unified National Coarse | 1/2″–13 UNC |
| UNF | Unified National Fine | 1/2″–20 UNF |
| UNEF | Unified National Extra Fine | 1/2″–28 UNEF |
| UN | Unified constant-pitch series, such as 8-UN, 12-UN and 16-UN | 1-1/2″–8 UN |
| UNS | Unified National Special | 1/2″–24 UNS |
| UNR | Unified thread with a rounded external root | Specify size, TPI and series |
| UNJ / UNJC / UNJF / UNJS | Unified J-profile threads, including coarse, fine and special series | Specify complete drawing designation |
| BSW | British Standard Whitworth, coarse | 1/2″–12 BSW |
| BSF | British Standard Fine | 1/2″–16 BSF |
| BSPP / G | British Standard Pipe Parallel | G 1/2 |
| BSPT / R | British Standard Pipe Taper; R denotes external taper | R 1/2 |
| Rc / Rp | BSP mating internal threads: Rc taper, Rp parallel | Rc 1/2 or Rp 1/2 |
| NPT | National Pipe Taper | 1/2″–14 NPT |
| NPTF | Dryseal National Pipe Taper | 1/2″–14 NPTF |
| NPSM / NPSL / NPSC | American straight pipe-thread series for different applications | Specify exact series |
| BA | British Association thread | 0 BA, 2 BA, 4 BA |
| BSB | British Standard Brass thread | Diameter × TPI BSB |
| BSC / CEI | British Standard Cycle / Cycle Engineers’ Institute | Diameter × TPI BSC |
| ACME | Inch trapezoidal thread, 29° profile | Diameter × TPI ACME |
| Stub ACME | Shallower ACME thread | Diameter × TPI Stub ACME |
| Tr | Metric trapezoidal thread, 30° profile | Tr20 × 4 |
| Buttress | Asymmetric thread for heavy axial loads | Specify standard and profile |
| Rd | Round thread | Specify standard, diameter and pitch |
Unified thread families are covered by ASME B1.1. This practical industry list includes common metric, Unified, British and pipe series; it is not every specialist thread standard worldwide.
Industrial uses
Illustrative industry applications, not customer or project claims. Discuss the drawing, material, machine, hole and production quantity with the manufacturer.
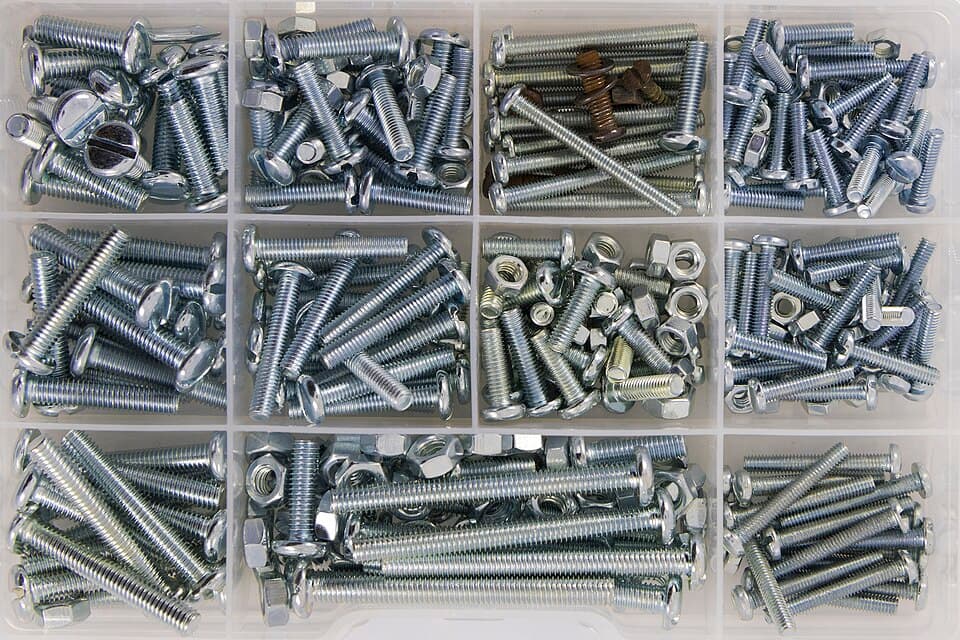
Internal threads in nuts and internally threaded components. Review a dedicated nut or machine tap for volume production.
Herusutimbul / CC BY-SA 4.0Discuss this application
Jigs, fixtures, die plates and tooling accessories where hardness, access and blind-hole clearance are suitable.
Discuss this application
Selected brackets and assemblies. Confirm special pitches, handedness and the exact component drawing.
Russ from Grosse Pointe Park / CC BY 2.0Discuss this application
Brackets, housings, fixtures and repair components. Distinguish manual work from repeated machine production.
Discuss this application
Machine components, assemblies and workshop fixtures matched to the material and thread depth.
Discuss this application
Mounting holes and threaded ports where parallel, taper and sealing requirements are confirmed.
Saud / CC BY-SA 4.0Discuss this applicationHSS long nut tap enquiry
Share the thread, material, machine, quantity, reach, coating or drawing reference. The enquiry is sent to the configured company inbox.
Buyer questions
It is used for suitable internal nut-threading operations where extended reach or component access needs to be considered.
Share thread, nut material, thread length, overall length, machine, quantity, tolerance and any drawing or gauge requirement.
Yes. Discuss the required coating and workpiece process so the available configuration can be confirmed.
Yes. Share the drawing, thread, length, tolerance, material, machine and quantity for a feasibility review.
Yes. Send a size-wise requirement list, grade, coating, repeat schedule and delivery requirements for quotation.
Continue exploring
Compare the short nut-tap route or review the wider threading range.
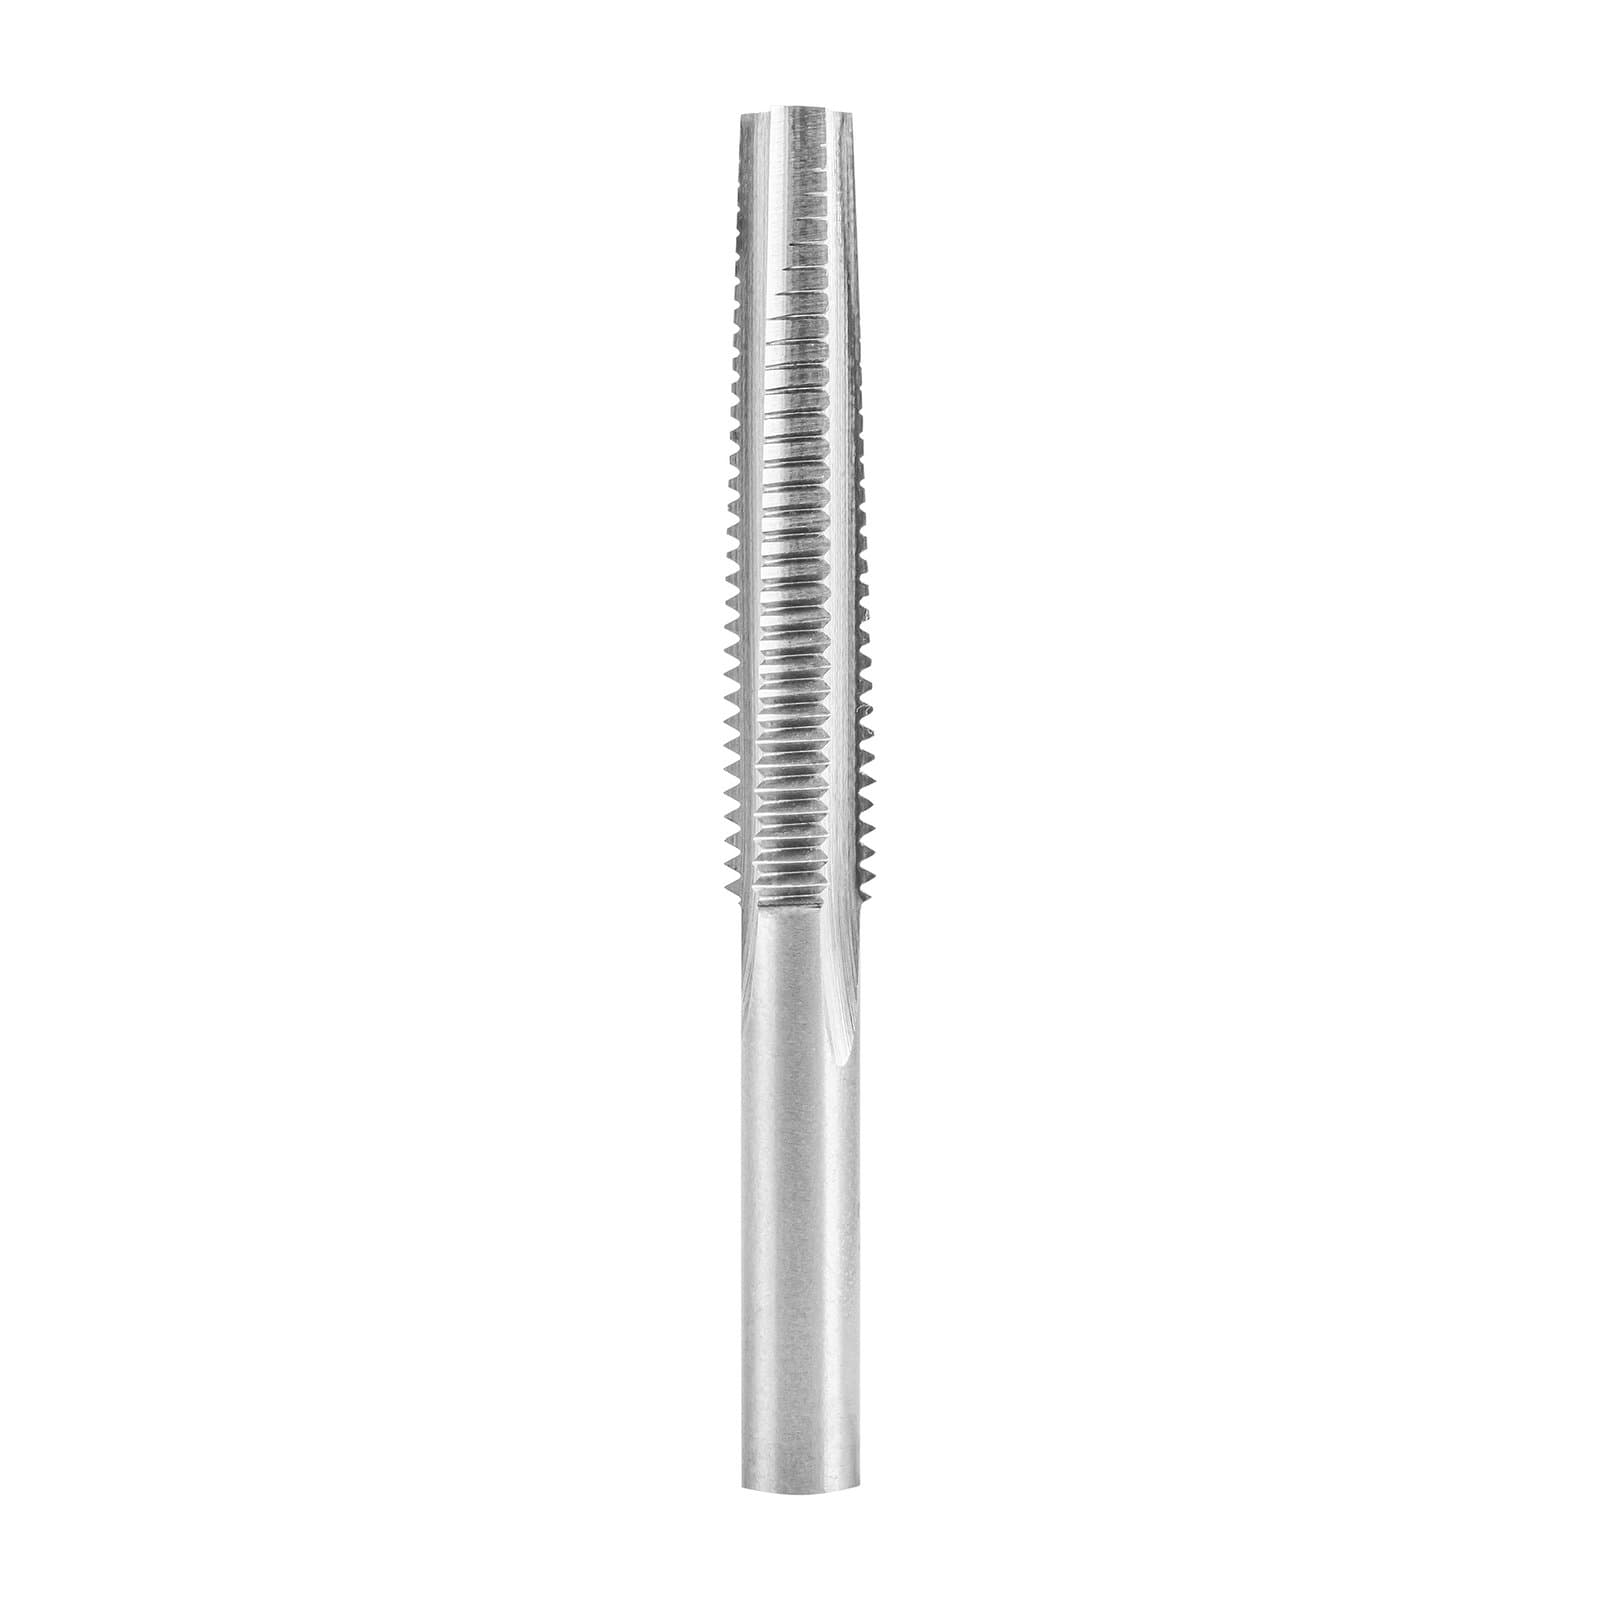 HSS Short Nut Tap
 HSS Machine Tap
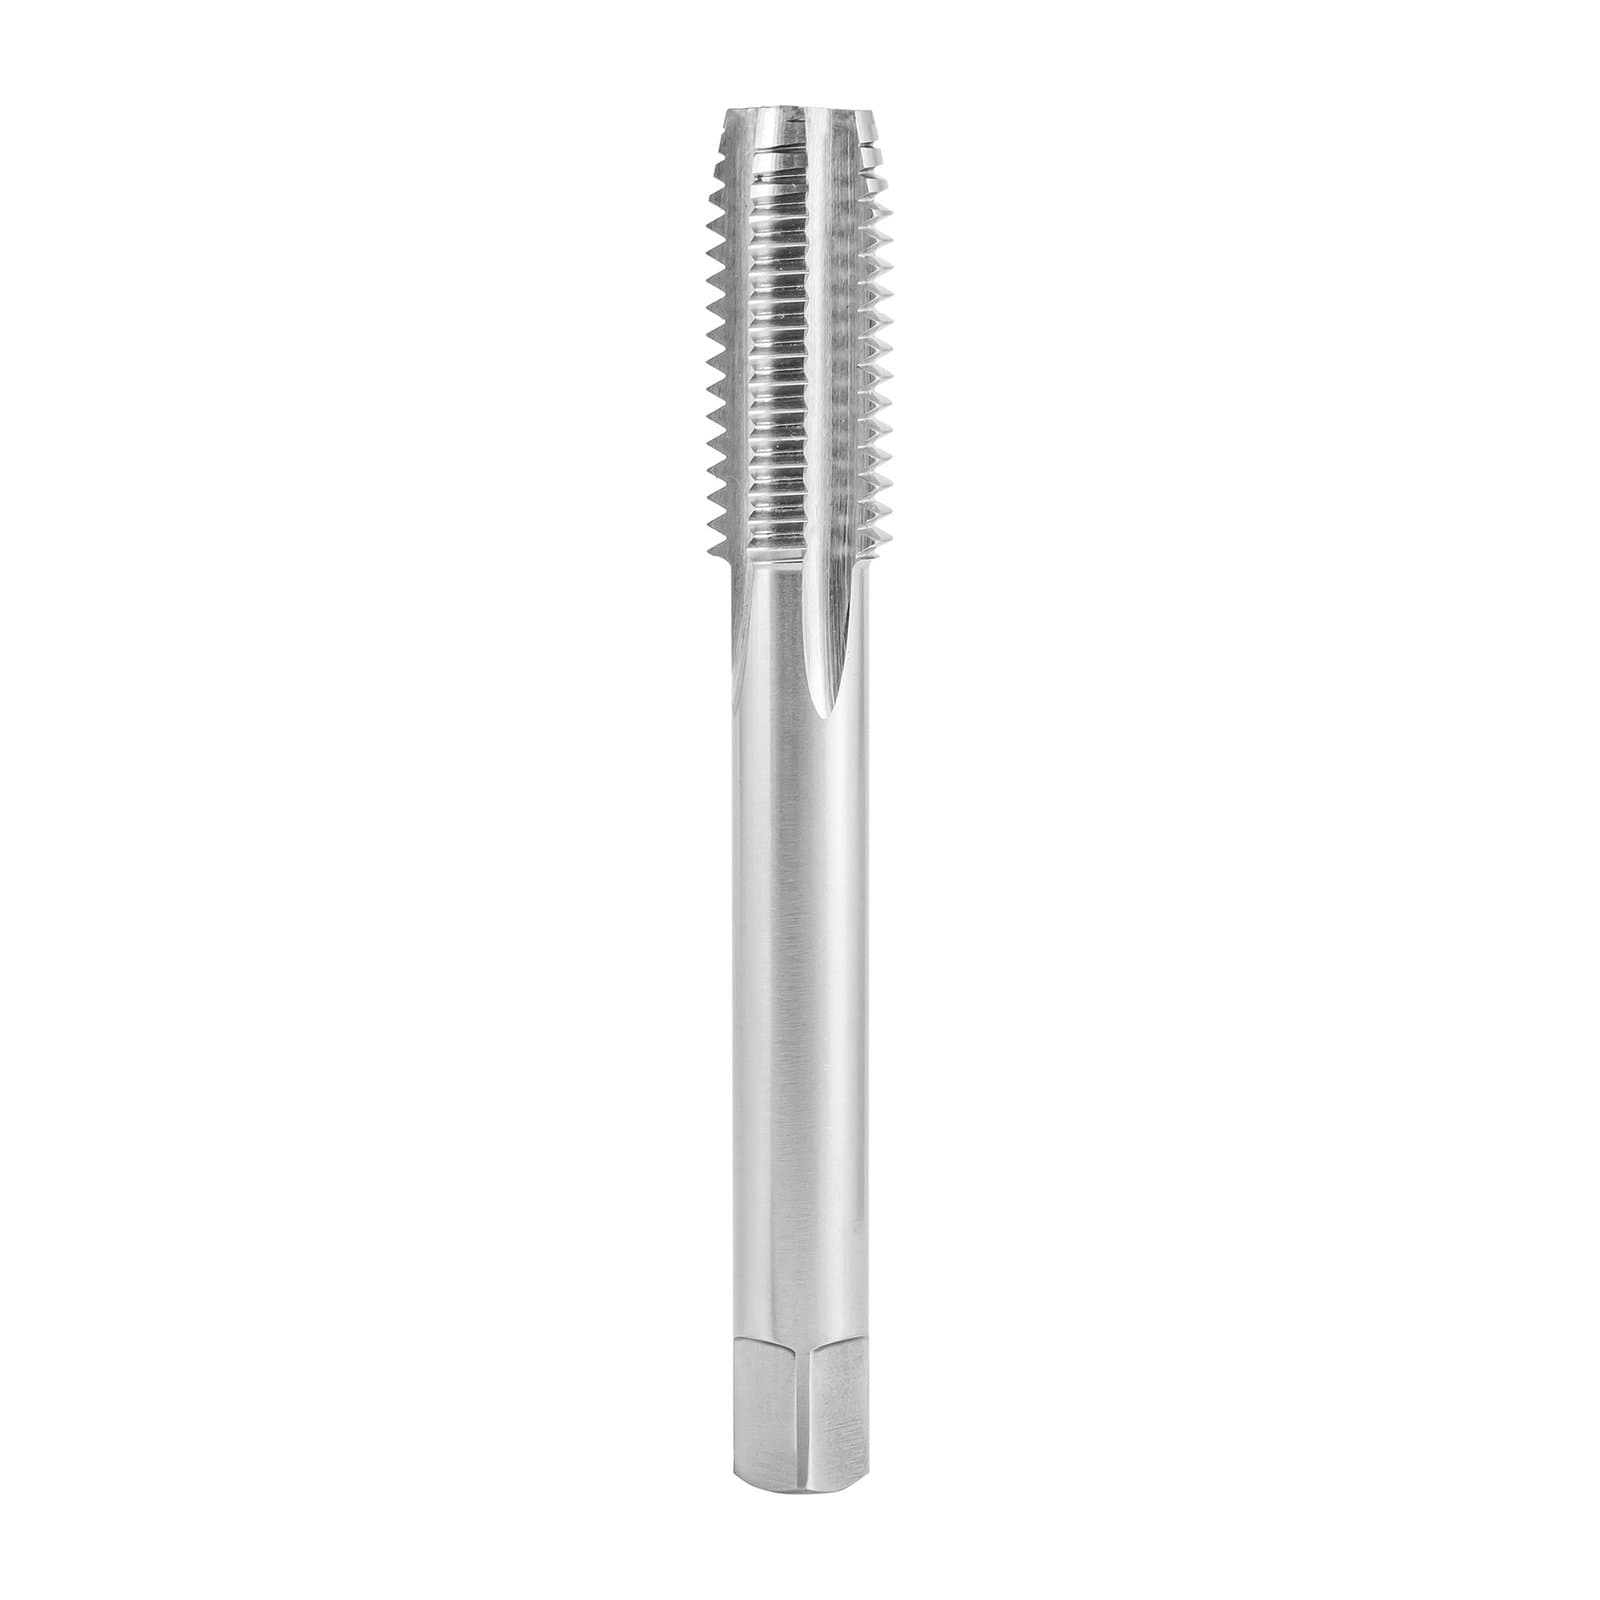 View all products